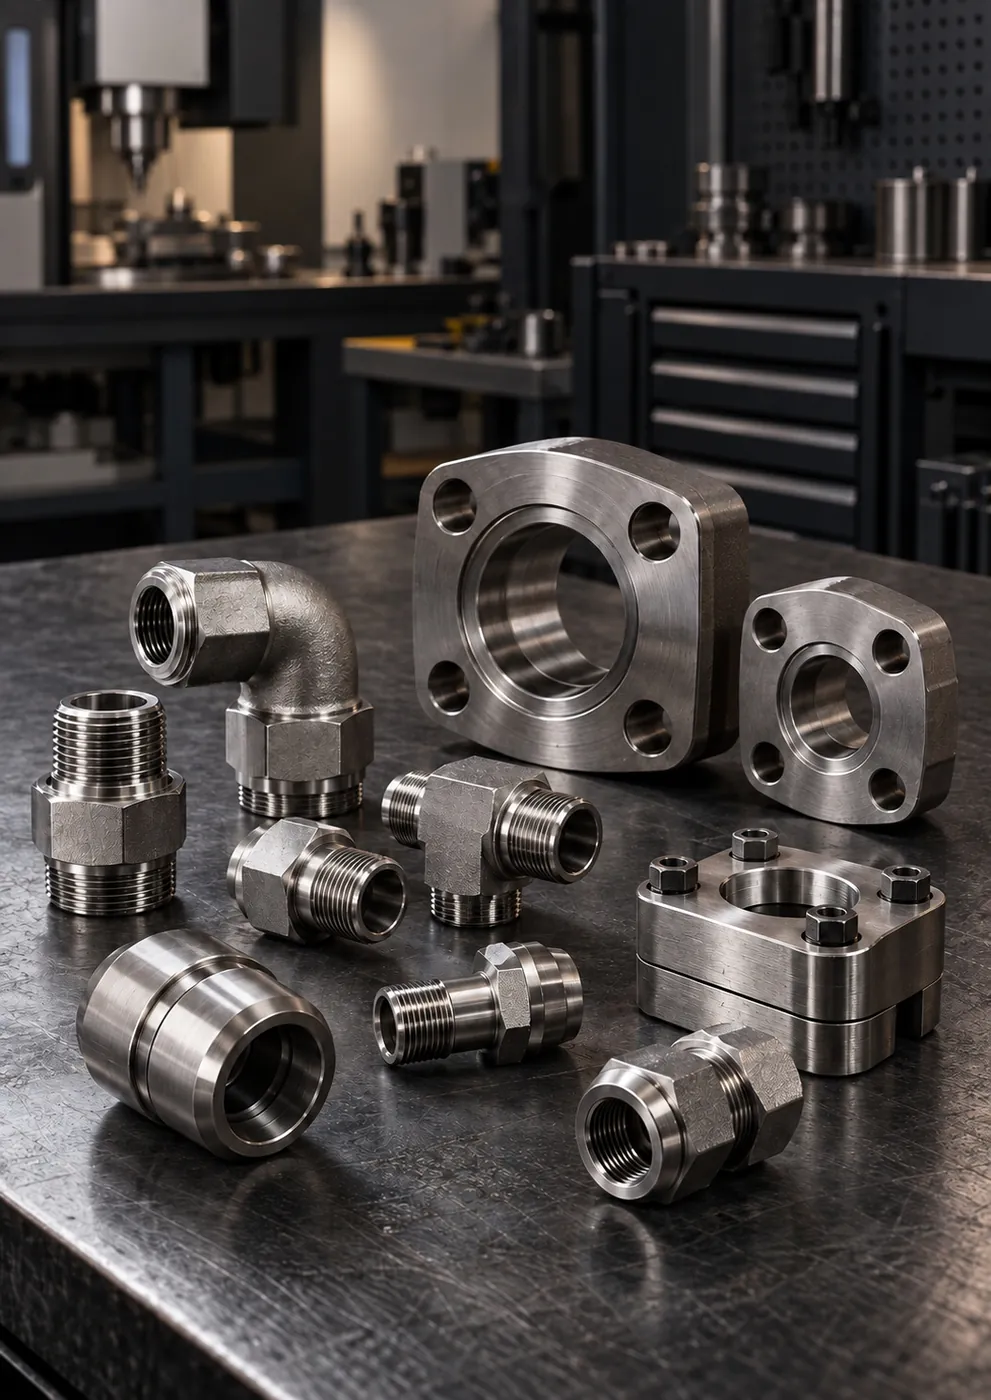
DIN 2353 Compression Fittings
Male Stud Connector (BSPP)
Stainless steel male stud connector with a 24° cone tube end and BSPP male thread, connecting tube to pump, valve block or…

High cycling · Heat · Emergency maintenance
High-pressure hose ends, SAE flanges and adapters built for the high cycling, heat and vibration of presses, mill rolls and hydraulic power units; supplied from stock for emergency maintenance.
Featured products in this sector
View all 23 productsProducts
23 products are listed for the operating conditions of Rolling Mills & Heavy Industry. Narrow down by group; open a product page for sizes and thread standards.
DIN 2353 Compression Fittings
Stainless steel male stud connector with a 24° cone tube end and BSPP male thread, connecting tube to pump, valve block or…

Hose Fittings & Ferrules
Stainless steel crimp-style 90° hose fitting with a female BSP swivel nut and 60° cone seat. Routes the hose at a right angle in…

SAE Flanges (Code 61 / 62)
Two-piece stainless steel split flange clamp that holds a flanged-head hose fitting or tube end against an SAE Code 61 port…

SAE Flanges (Code 61 / 62)
Stainless steel flange block combining SAE flange ports in a single body with elbow, spacer, reducer or distribution functions…

Custom-Made Hydraulic Parts
Custom stainless hydraulic adapter CNC-machined from a sample or technical drawing for thread, size and angle combinations not…

DIN 2353 Compression Fittings
24° cone straight coupling (DIN 2353) that joins two stainless steel tubes on the same axis without welding. AISI 316L body, L…

DIN 2353 Compression Fittings
Stainless steel 24° cone equal elbow providing a weld-free 90° change of direction in a tube line. For tight installation spaces…

DIN 2353 Compression Fittings
Stainless steel 24° cone equal tee joining three tubes of the same diameter, used to branch off the main line. AISI 316L, DIN…

Hose Fittings & Ferrules
Stainless steel O-ring face seal (ORFS) hose fitting with a female swivel nut. Reduces the risk of leaks in high-pressure lines…
Hose Fittings & Ferrules
Stainless steel crimp-style 90° hose fitting with an SAE Code 61 flange head. Connects to pump and block ports in large-bore…
Hose Fittings & Ferrules
Stainless steel DKOL straight hose fitting (L series) with a metric swivel nut and 24° cone with O-ring. Connects directly to DIN…

Hose Fittings & Ferrules
Stainless steel crimp ferrule for 2SN hydraulic hoses with two steel wire braids. Crimped together with the hose fitting to form…
Hose Fittings & Ferrules
Stainless steel ring-type (banjo) hose fitting connected to the port with a hollow bolt. Rotatable connection perpendicular to…

SAE Flanges (Code 61 / 62)
Stainless steel SAE Code 62 mating flange for high-pressure hydraulic lines. Connects the pipe to a Code 62 port via a welded or…

SAE Flanges (Code 61 / 62)
Stainless steel blind flange for closing off unused SAE flange ports or flanged line ends. Made to Code 61 and Code 62 port…
JIC 37° Fittings & Adapters
Stainless steel conversion adapter with a JIC 37° UNF male end and a BSPP parallel male thread. For connecting JIC hose lines to…
BSP / NPT Adapters & Nipples
Stainless steel male x male reducing adapter with BSPP threads of different sizes and a 60° cone seat at each end. Size…

BSP / NPT Adapters & Nipples
Stainless steel hex head plug with a BSPT tapered thread for closing unused female ports and threaded line ends. AISI 316L.
BSP / NPT Adapters & Nipples
Stainless steel BSPP reducing adapter with parallel threads, sealed on the port side by a bonded seal. For ports that are opened…
Weld Nipples & Weld Fittings
Stainless steel set consisting of a 24° cone body, a nut and an O-ring weld nipple that is butt-welded to the tube. Adds a…
Weld Nipples & Weld Fittings
Stainless steel 90° elbow with one end welded to the tube and a 24° cone bite-type compression end on the other. Right-angle…
Weld Nipples & Weld Fittings
Stainless steel 24° weld nipple that is butt-welded to the tube end and seats in a 24° cone with an O-ring. Straight, reducing…

Custom-Made Hydraulic Parts
Stainless steel manifold blocks machined from solid to technical drawings, combining multiple hydraulic lines in a single body…
Can't find your part in the list?
Send a sample photo, technical drawing or dimensions; we'll identify the right fitting from our catalog or through custom manufacturing.
Faik Güney · Contact person
Services
Beyond supplying parts, we complete the job in the field with piping, hose assembly, custom manufacturing and technical identification.
Hydraulic hose assembly and crimping: hose assemblies with straight, 45° and 90° stainless steel ends in BSP, JIC, NPT…
View service – Hydraulic Hose AssembliesStandard stainless steel fittings, adapters, hose ends, flanges and valves ready to ship within an average of 1-3…
View service – Fast Supply & Shutdown SupportOrderly, labeled and service-friendly connections with stainless steel tube and fittings on control panels, power units…
View service – Control Panel & HPU TubingWhere a standard product is not the answer: custom adapters, nipples, flange blocks and transition parts made from a…
View service – Custom Parts from Drawings & SamplesThread profiles, sealing cones, wrench flats and connection geometry are machined from AISI 316/316L bar on CNC…
View service – Stainless Steel CNC MachiningIdentifying BSP, NPT, UNF/JIC and metric threads by measurement, matching them correctly to the mating part, and…
View service – Fitting & Thread IdentificationWelded and demountable stainless steel lines built from AISI 316/316L pipe, flanges and fittings: bevel preparation…
View service – Stainless Steel Pipe FabricationSelection of AISI 316L-body ball valves, needle valves and check valves by body, connection standard, bore size…
View service – Valves, Check Valves & Flow ControlOverview
Quick answer
Rolling mills use high-pressure hose ends, SAE Code 61/62 flanges and adapters on press, mill roll and hydraulic power unit lines. Selection is based on hose size, flow rate, pressure class and bend radius. For emergency maintenance, plan for frequently replaced hose ends and adapters to be supplied from stock (typically 1-3 business days), made-to-length hose assemblies within an average of 5-15 business days, and custom blocks and sizes within an average of 10-20 business days after technical approval.
In a rolling mill, hydraulics are the muscle that keeps the line running nonstop. The cylinders that set the roll gap, the presses, the shears and the power units go through repeated pressure build-up and release on every shift. Radiant heat from hot stock, cooling water and mill scale put these connections under constant stress. Presses, mill rolls and hydraulic power units need a fitting layout that can withstand high cycling, heat and vibration.
GÜNEYSS supplies high-pressure hose ends, SAE flanges, flange blocks and adapters to rolling mills, metalworking plants and heavy industry operations. In emergency maintenance situations, frequently replaced hose ends, adapters and flanges are supplied from stock; made-to-length hose assemblies are prepared within an average of 5-15 business days, and custom blocks and non-standard sizes within an average of 10-20 business days after technical approval.
Field conditions
We select fittings for these conditions and specify the material, sealing type and installation method accordingly.
Describe your own conditionsFittings fatigue in circuits where pressure constantly builds and releases; selection must go beyond nominal pressure.
Rapid valve movements and shock loads create momentary pressure spikes in the line.
Hoses and seals near hot stock age prematurely due to heat.
The wet, abrasive environment rusts carbon steel fittings and seizes their threads.
A single hose failure stops the line; a spare in the right size must be found fast.
Presses and roll drives loosen fittings, making clamping and support layout critical.
Technical selection notes
Points we clarify with you before ordering for Rolling Mills & Heavy Industry applications.
An undersized hose leads to high flow velocity, heat buildup and pressure loss.
Choose the pressure class based on impulse and cycle loading, not just working pressure.
Routing below the minimum bend radius fatigues the reinforcement layer.
On large-diameter high-pressure lines, flanges are easier to install and remove than threaded connections.
Sizes of frequently replaced hose assemblies and adapters should be recorded in the maintenance plan and kept in stock.
Detailed guide
In rolling mill hydraulics, what stresses a connection is often not the nominal pressure but how often and how quickly the pressure changes. Rapid valve opening and closing and shock loads create momentary pressure spikes in the line above the nominal value. For this reason:
Pressure spikes are often caused by sudden valve closure, a cylinder bottoming out hard at end of stroke, or an incorrect accumulator precharge pressure. Investigating these causes, not just replacing the fitting, prevents the same failure from recurring shortly afterwards.
On hot rolling lines, fittings are exposed both to radiant heat from the hot stock and to a mixture of roll cooling water and mill scale. Carbon steel fittings rust quickly in this wet, abrasive environment; a fitting that needs to come off during maintenance ends up seized on its threads. AISI 316/316L stainless steel fittings greatly reduce external corrosion and thread seizure. Hoses close to a heat source should have a heat-protective sleeve and a suitable hose type, and should be routed as far from the hot zone as possible.
When assessing a hose's operating temperature, fluid temperature must be taken into account as well as ambient temperature. Hot oil ages the hose inner tube and the seals; inadequate cooling in the power unit is one of the overlooked causes of recurring leaks at fittings.
Rolling mill power units consist of high-flow pumps, filter assemblies and accumulator stations. Pump outlets and main pressure lines are usually connected with SAE flanges, while at manifold outlets, flange blocks, elbows and adapters make up the line layout. A custom-size flange block can combine a chain of several elbows and adapters into a single part, reducing both the number of potential leak points and the installation space required. On accumulator connections, isolation and bleed points should be planned in advance so that pressure can be safely released during maintenance.
| Criterion | Consequence of a wrong choice |
|---|---|
| Hose inside diameter and flow rate | High flow velocity, heat buildup and pressure loss |
| Pressure class | Premature failure under impulse loading |
| Bend radius | Fatigue of the reinforcement layer and failure at the hose end |
| Twisting | Significantly shorter hose life |
| End angle and length | Hose running under tension or abrading |
When the end angles (straight, 45°, 90°) and length of a hose assembly are selected correctly, the hose works without stretching or twisting as it moves, which directly extends its service life.
Mill scale and dust mostly get into the hydraulic circuit during maintenance. Capping removed hose and fitting ends immediately, keeping new parts in their protective caps until installation, and cleaning the connection surfaces before assembly eliminates a major source of valve and pump failures. On stainless steel threads, a suitable anti-seize compound should be used during assembly to prevent galling, and flange O-rings must be seated correctly in their grooves. Checking the filter condition after any intervention that opens the line limits the spread of contamination introduced during maintenance. A controlled leak check should be carried out after initial commissioning.
In a rolling mill, the cost of an unplanned shutdown far exceeds the cost of the part. That is why we recommend that maintenance teams draw up a size list for the most frequently replaced hose assemblies, adapters and flange O-rings and keep critical sizes in stock. For emergency maintenance, stocked hose ends, adapters and standard sizes are typically ready to ship within 1-3 business days, while hose assemblies crimped to length are prepared within an average of 5-15 business days. Custom flange blocks and non-standard sizes are manufactured within an average of 10-20 business days after technical approval. Worn or damaged custom parts can be remanufactured from a sample or technical drawing. For urgent requests, sending the connection type at both ends, end angles, hose inside diameter, length and working pressure together ensures that the right part is prepared the first time.
Applications
Teams in Rolling Mills & Heavy Industry that need fittings, hose assemblies and custom parts.
Roll gap adjustment and balance cylinders, power units and material handling hydraulics.
High-pressure hose ends and SAE flanges on press, shear and straightening lines.
Flange blocks and adapters for presses operating under shock loads.
Stainless steel fittings for heat-exposed lines in die and handling hydraulics.
Emergency supply of hose assemblies and adapters for heavy industry customers.
Pump outlet, manifold and accumulator connections for high-flow units.
Gallery
Knowledge Center

Stock items are prepared within an average of 1-3 business days, standard production within 5-10 business days, hose assemblies made to length within…

The right hose assembly is defined by seven pieces of information: inside diameter and length, temperature, application conditions, fluid, working…

Hydraulic connections are sealed in four ways: O-ring, bonded seal (Dowty washer), metal cone face and tapered thread. On parallel threads, the seal…
Frequently asked questions
If your question isn't answered here, write to us and we'll pin down the size, thread standard and material together.
Send us your questionStocked hose ends, adapters and standard sizes are typically ready to ship within 1-3 business days; if a ready-made hose assembly in the same size is in stock, it is also shipped within this time. Hose assemblies crimped to length are prepared within an average of 5-15 business days, depending on end type, quantity and hose stock availability. If you send us the connection type at both ends, end angles, hose inside diameter, length and working pressure by phone or WhatsApp, we will quickly confirm stock availability and give you a separate lead time for any assembly that needs to be built. Keeping spares on site for hoses that fail frequently is the measure that cuts downtime the most.
SAE flanges are preferred on large-diameter high-pressure lines; at these sizes, threaded connections require very high tightening torque and carry a risk of thread damage during removal. The choice between Code 61 and Code 62 depends on nominal size, working pressure and port geometry.
The most common causes are routing below the minimum bend radius, installing the hose twisted, and choosing the wrong end angle or length. Impulse loads that are high relative to the hose's pressure class also shorten its life. If you share a photo of the current routing, we can assess it and suggest an end angle and length.
Yes. Port dimensions, bolt pattern, O-ring groove and connection orientation are verified from a sample or technical drawing, and production begins after first article approval. Custom blocks and sizes are manufactured within an average of 10-20 business days after technical approval.
In areas with heavy exposure to cooling water, mill scale and moisture, carbon steel fittings rust quickly and come off with seized threads during maintenance. Stainless steel fittings greatly reduce external corrosion and thread seizure, shortening removal and replacement time. In dry, sheltered areas, the need can be assessed case by case.
Quote
Send us the sizes of your frequently replaced hose assemblies, adapters and flanges; we'll tell you separately which can be supplied from stock and which require manufacturing, with lead times.
Rolling Mills & Heavy Industry request form
Other sectors